
Published: 2026-09-06 | Technical topic: main drive fault diagnosis on KBA presses. A main drive that fails to start, trips during running, shows speed fluctuation or overcurrent alarms should not be handled by repeated resetting. Preserve the alarm state, isolate safely, then separate three classes of problem: the drive refuses to start, the drive trips after starting, or the drive runs normally but the mechanical load cannot be driven. Confirm model, serial number, drive version and site modifications against the documentation; these checks do not replace the manufacturer's latest technical requirements.
Safety note: before opening the electrical cabinet, checking motor wiring, touching the DC bus, removing resistors or entering the cylinder and drive areas, shut down and disconnect the main power using the stop procedure, apply lockout/tagout, close relevant air supplies, and verify residual voltage has fallen to a permitted value with a suitable meter. Braking resistors, the DC bus and motor windings may hold dangerous energy after shutdown. For barring, couplings, drive shafts and cylinders, confirm that mechanical inertia, pneumatic and hydraulic energy have been released.
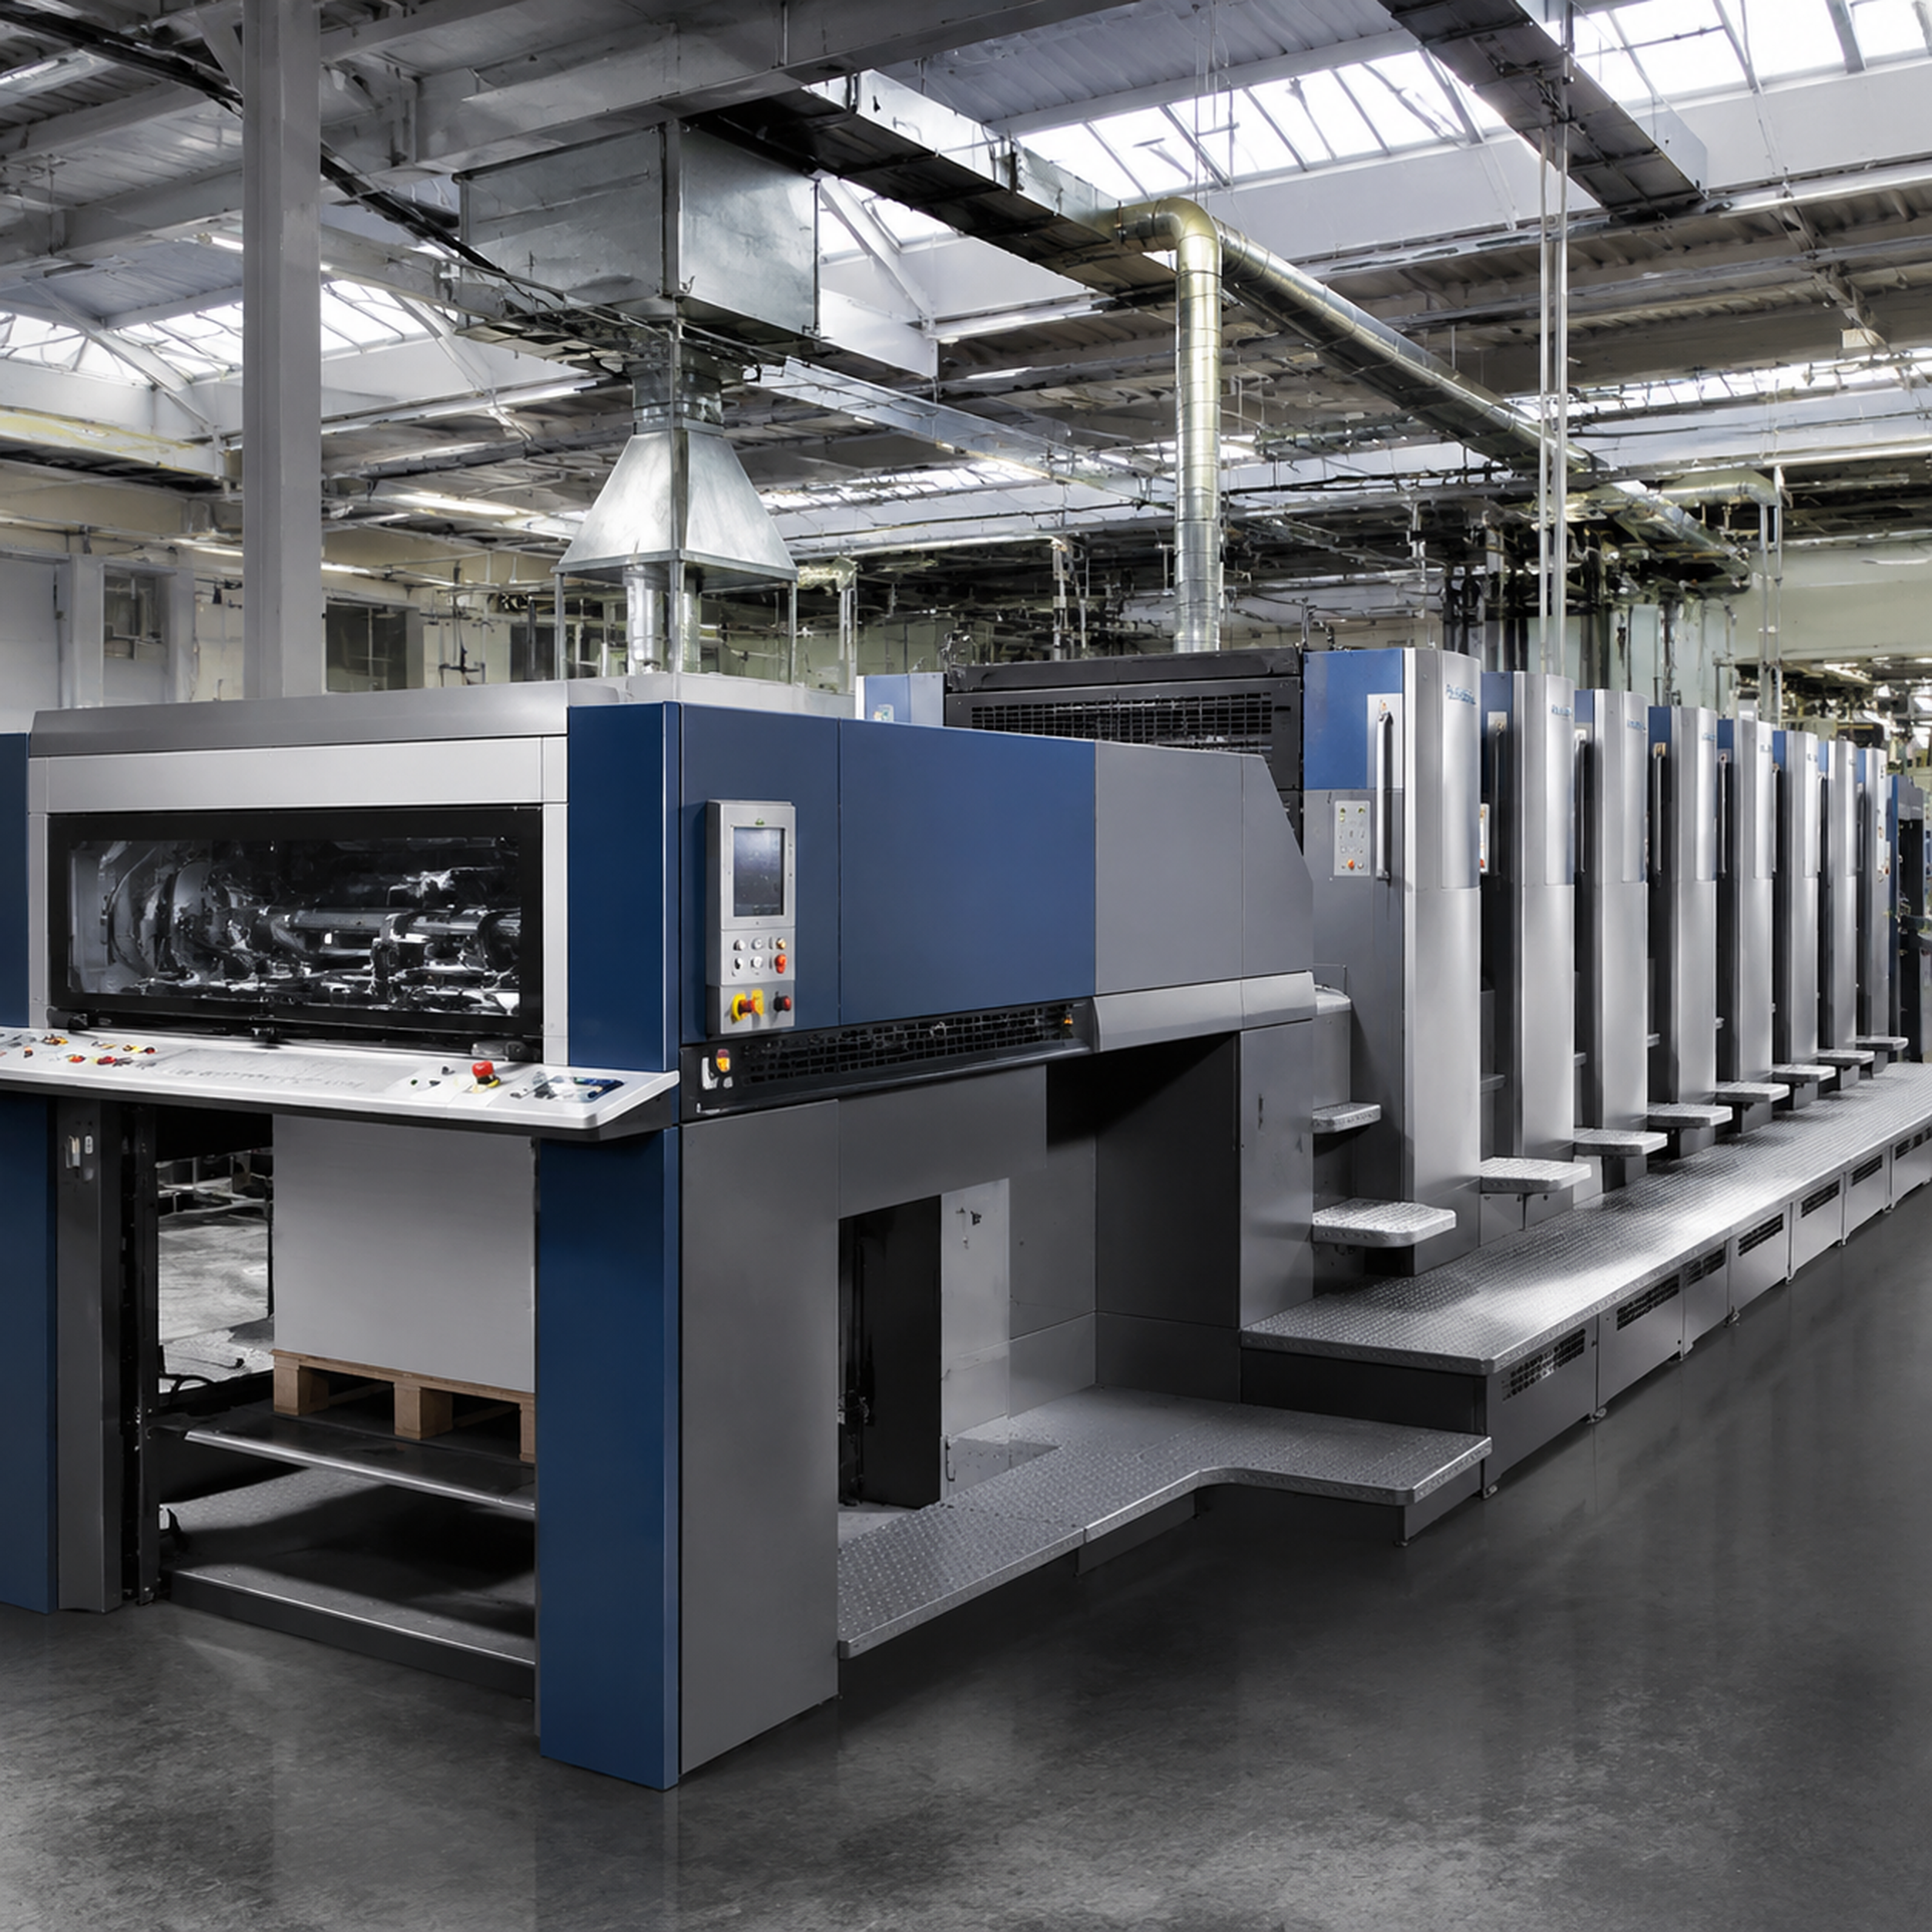
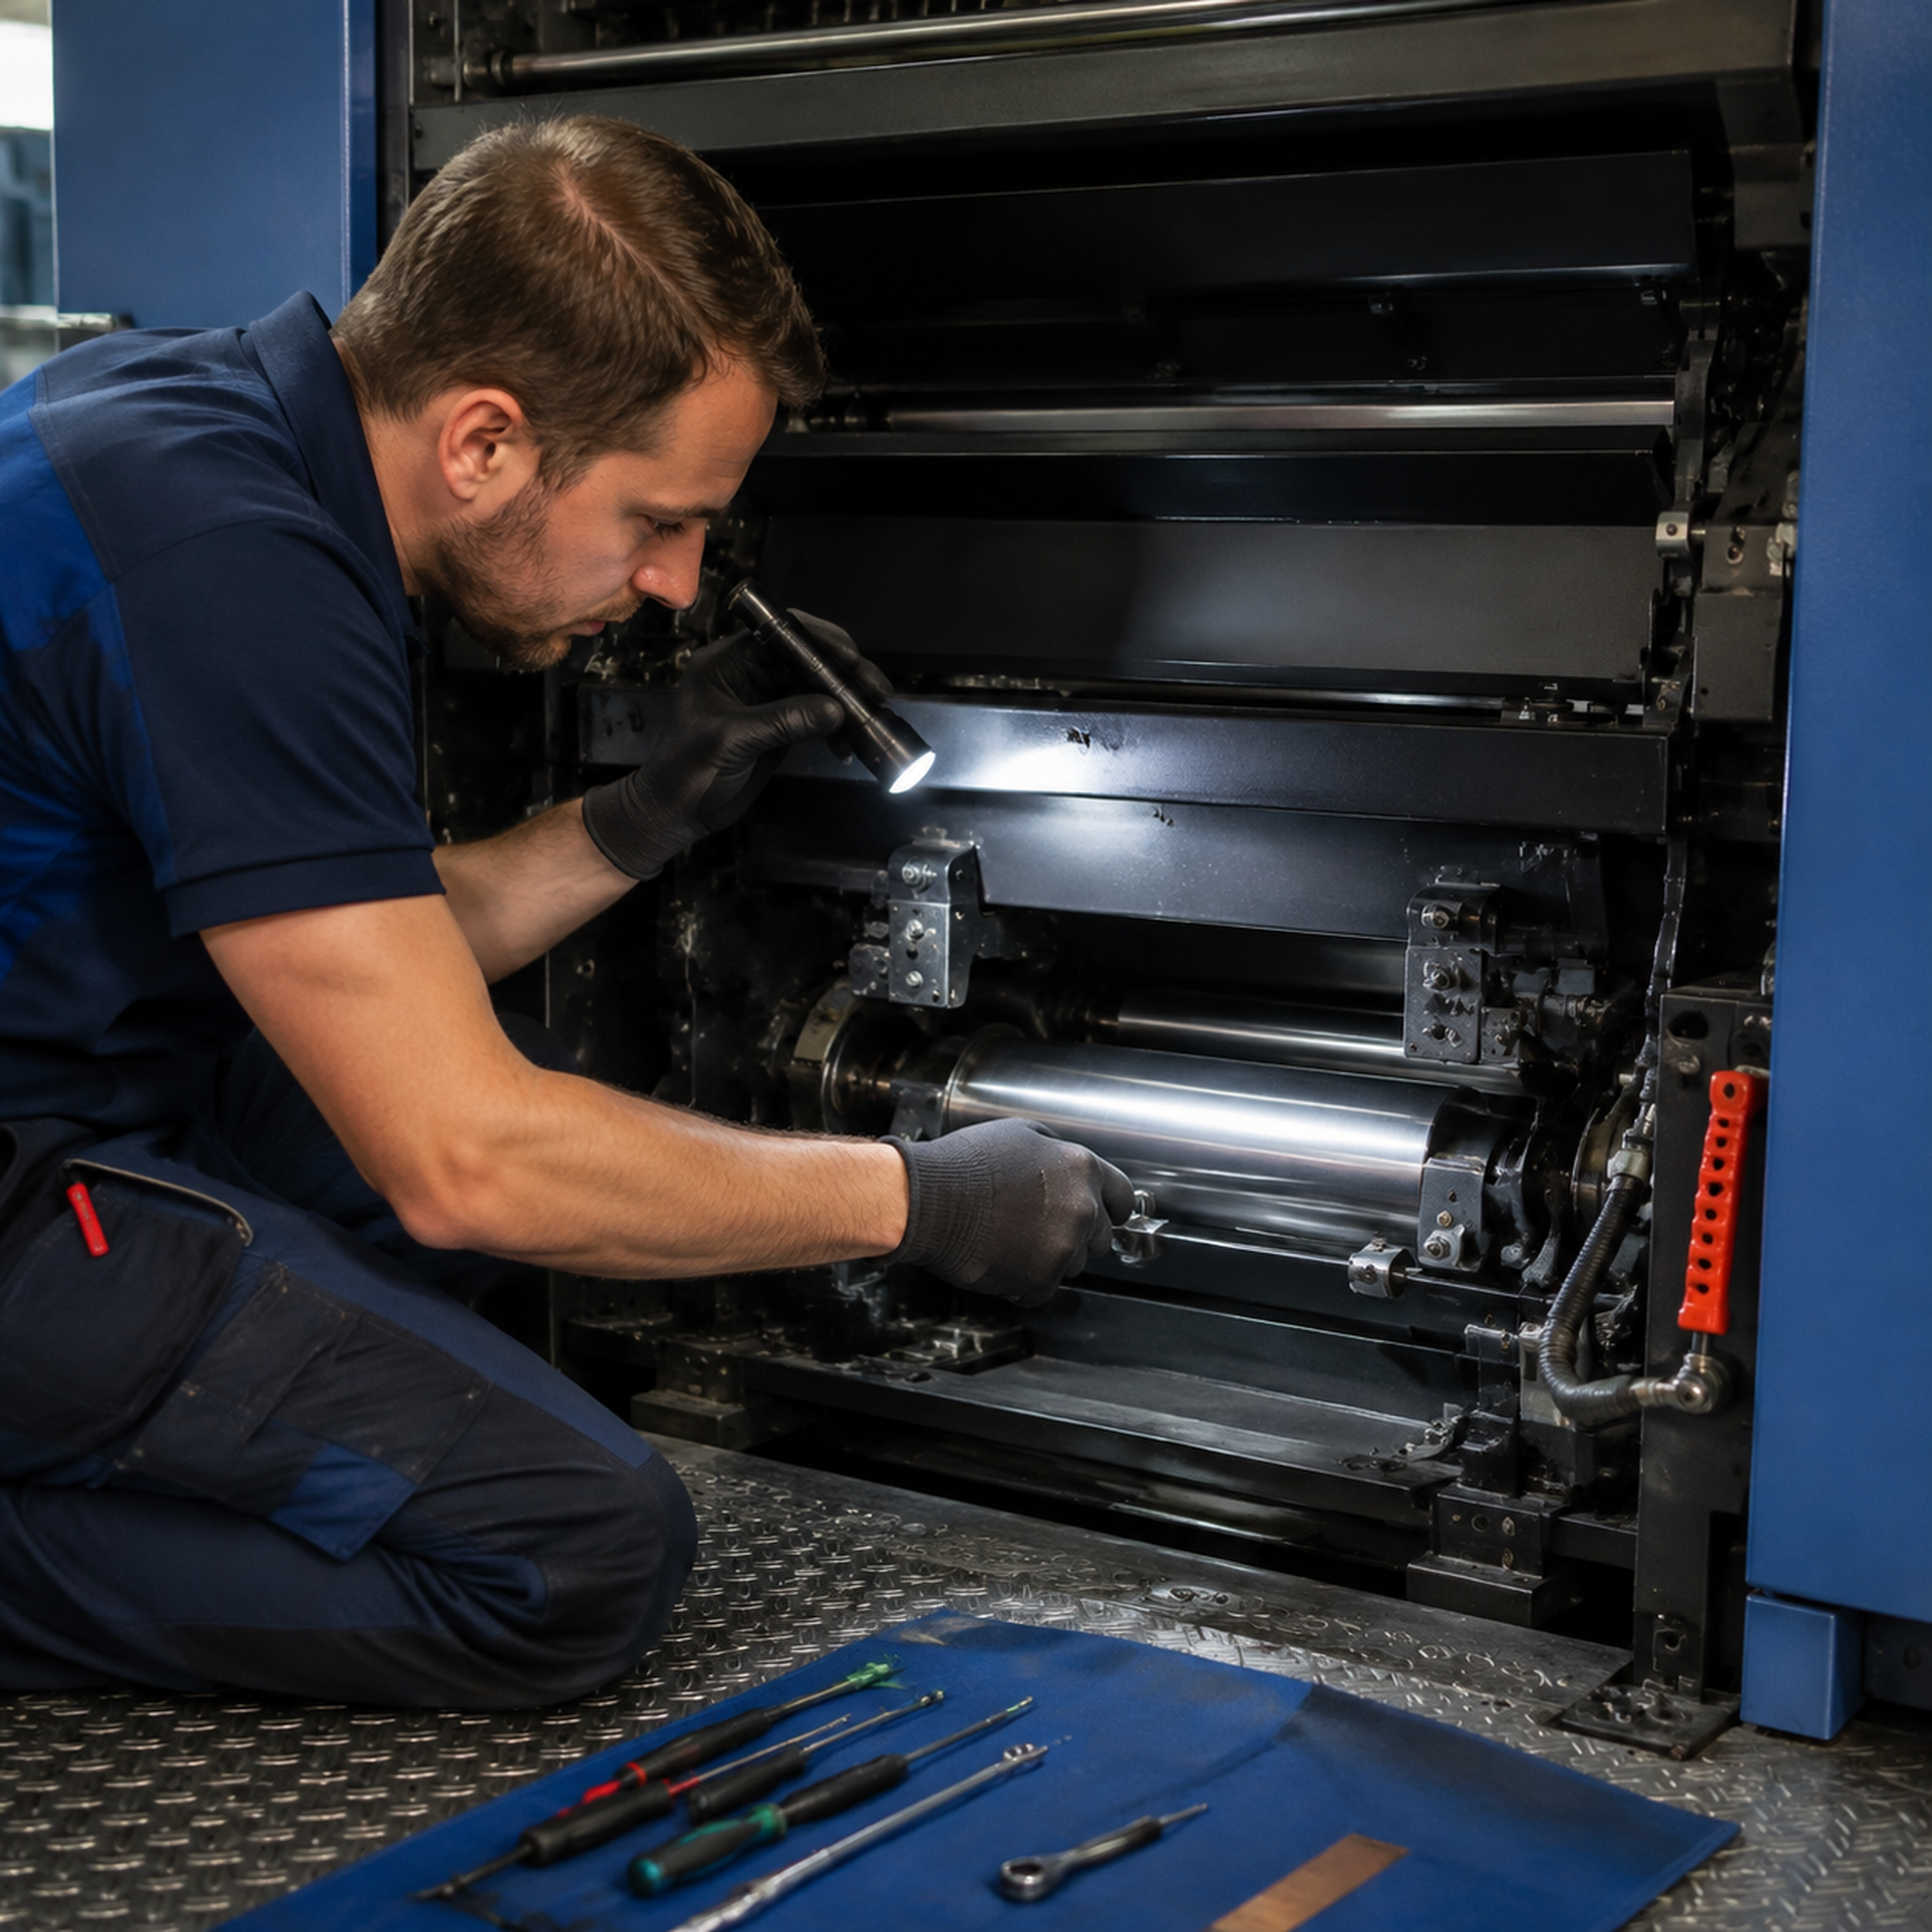
AI-generated image: main drive repair inspection on a KBA press. Not a real customer-site photograph.
1. Build the fault boundary from the alarm behaviour
On start failure, record the alarm code, time and conditions from the operator panel, drive display and higher-level control system. Do not just record "overcurrent": note whether the machine was idling, printing, feeding, accelerating or braking. If the alarm appears immediately after pressing start, check the start-permit, emergency-stop circuit, interlocks, drive enable and motor cable first. If it appears after several minutes of running, put temperature rise, ventilation, mechanical friction and load changes first.
A trip immediately on start points to the permit circuit, short circuit, earth fault or parameter range; confirm no obvious short at the motor terminals and save the alarm record. Normal at low speed but overcurrent when accelerating points to mechanical load, acceleration time or feedback; compare current and torque trends at different speed ranges. Alarms after the machine is warm point to cooling, fans, bearings or braking resistors; record the cold-to-hot temperature difference. Speed fluctuation points to the encoder, feedback cable, control parameters or coupling; check for lost pulses or jumps in the feedback state.
2. Check the power circuit and motor-side condition
After energy isolation and safety confirmation, inspect the drive input and output terminals, motor junction box, earth connections and cable sheaths. Look for discoloured or loose terminals, correctly connected shielding, and cables pinched in cable tracks, entry points or after previous repairs. When measuring motor winding insulation or phase condition, use methods suited to the drive and motor system, and disconnect electronic components that could be damaged by high-voltage testing.
If the drive reports an output fault as soon as it is enabled, do not conclude that the power module is damaged. Moisture in the motor cable, contaminated terminals, an unreleased brake or mechanical jamming can produce the same behaviour. Separate the motor side from the drive side where the equipment allows, and let qualified electrical personnel decide whether power-module and motor insulation tests are appropriate.
Include the braking resistor and cooling path in the check. If the resistor shows obvious overheating marks, loose terminals, or the air path is blocked by paper dust, do not keep producing by lowering the alarm threshold. A stopped fan, blocked filter or high cabinet temperature can push a normal drive into thermal protection during continuous production or frequent acceleration and braking.
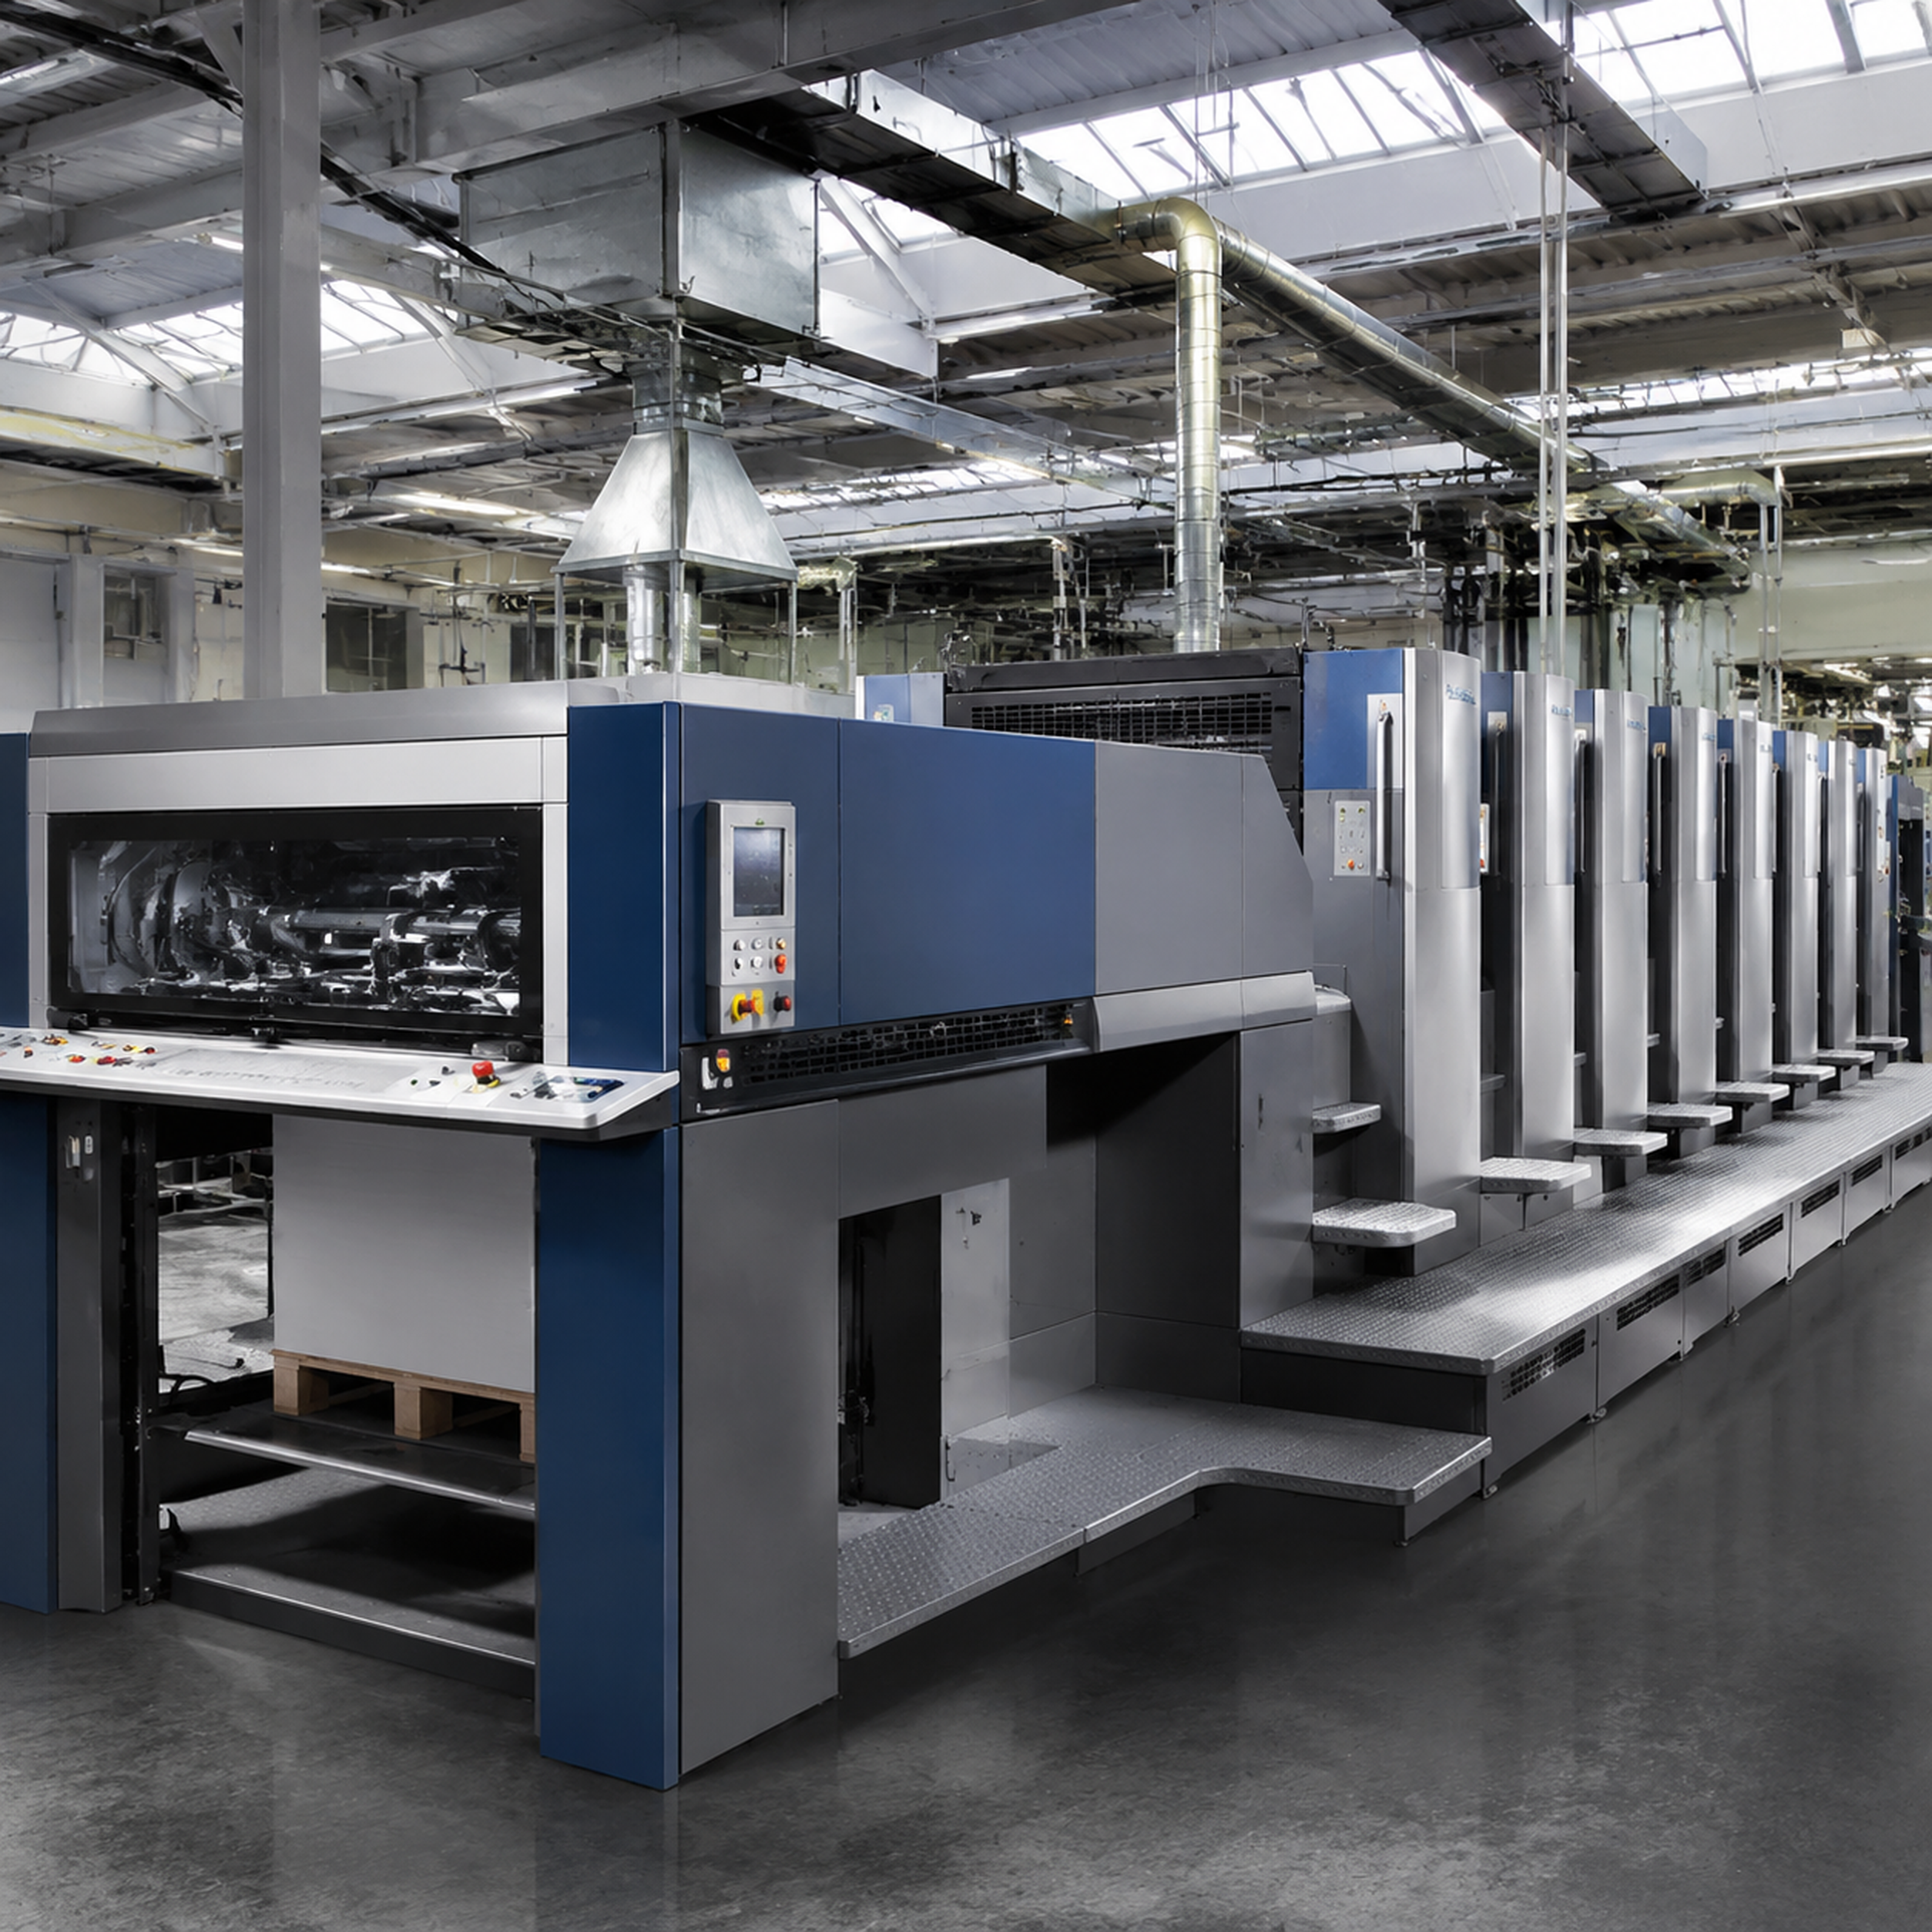
AI-generated image: press drive train and electrical control inspection. Not a real customer-site photograph.
3. Mechanical load is the other main line in overcurrent faults
Main drive overcurrent is not always electrical. After stopping and locking out, check the main motor coupling, drive shaft, gear meshing, cylinder nip and the running resistance of auxiliary pumps and fans. After a jam, foreign object entry, poor lubrication or bearing damage, the drive raises current to hold speed and finally trips during acceleration or running.
For a mechanical load check, first confirm that cylinders and drive parts can be safely barred by the prescribed method, then look for a sudden rise in resistance at a certain angle, periodic rubbing noise or coupling runout. Do not jog the machine to verify the fault, and do not remote-start while guards are removed or personnel are near pinch points. If cylinder clearance, impression pressure or gear reference may have changed, have service personnel familiar with the model continue.
Abnormal barring resistance when empty: check mechanical interference, bearings, gears and lubrication. Normal when empty but current rises quickly after impression: check impression, cylinder clearance and related actuators. Periodic current fluctuation at a particular speed range: check the coupling, encoder feedback and rotating-part balance. Noise and temperature rise together after a repair: stop and re-check the assembly, do not "run in" with extended operation.
4. Verify parameters and feedback signals item by item
After replacing a drive, control board, memory module or motor, the most common problem is "hardware replaced but the parameter set does not match". Keep the original parameters and version information first, then check motor rated current, maximum armature current, braking current, excitation-related parameters, acceleration and deceleration times, speed reference and feedback direction against the equipment configuration. Different power combinations cannot share one set of values; current-capture and load parameters must match the actual motor, drive and modification state.
For parameter writes, program downloads or controller resets, use matching maintenance tools and versions and connect interfaces in a de-energised state. Record values before and after each change, the operator and the trial result. If replacing a memory module or control program, back up the original data first, then load the operating system, user program and equipment data; do not overwrite the current device with a neighbouring machine's files.
AI-generated image: main drive parameter verification. Not a real customer-site photograph.
5. Restart must be verified in stages
Do not return to production speed immediately after the fault is cleared. Before restarting, check that no tools remain in the cabinet, guards, covers, earth connections, looms and pipes are restored, and the emergency stop and interlocks work. On first power-up, only observe the control system and drive state, confirm no abnormal smell, sound or fast temperature rise, then run at low speed or empty per the machine rules and observe current, speed feedback, vibration and braking.
Run empty at low speed and confirm start, stop, acceleration and deceleration produce no alarm. Run at low speed with paper and check whether feeding, impression, registration and delivery are affected by the main drive restoration. Raise gradually to the normal speed and record current, temperature, feedback speed and alarm state. After stable continuous running, sample print quality and unit synchronisation. Write the fault code, measurements, adjustments, replaced parts and acceptance results into the maintenance record.
Reminder: barring, jogging and releasing the brake must be done by trained personnel. Keep hands and body away from cylinder nips, couplings, gears and chain pinch points. Do not run production with any guard removed or interlock bypassed.
Conclusion
Effective handling of KBA main drive faults is not about pressing reset faster, but about putting the alarm information, power circuit, mechanical load, parameter set and feedback signals on one diagnostic chain. Lock the risk first, then separate the fault boundary, and finally accept stage by stage through low speed, paper feed, speed increase and continuous running to reduce repeated trips and wrong parts replacement. The workshop can convert this sequence into a machine inspection sheet and record current, temperature and alarm trends to turn unplanned stops into planned maintenance tasks.
Images are schematic illustrations of repair scenarios to show inspection positions and sequences; they do not represent any specific customer site.